
60MW Confidential Client, Greenfield Data Center AI Liquid-Cooled Rack Test Campus – Texas
Project Overview
- $390 Million Construction Cost
- 60 MW Campus Electrical System Capacity
- Liquid Cooled Racks + Hot-Aisle/Cold-Aisle Containment
- 2 Test Lines
- 262 Rack Test Positions
- SMT Manufacturing, Sub-Assembly and Liquid-Cooled Rack Test
Project Overview
Summit designed the mechanical, electrical, plumbing and controls systems for a new-build, ground-up manufacturing, assembly and test facility. The manufacturing floor carries four parallel surface-mount technology (SMT) lines, two processor-board lines with dedicated ovens and X-ray inspection, general rework and board-rework areas, and support rooms including a humidity-controlled room, SMT spares and SMT programming areas.
For the high-electrical demand system, Summit coordinated with the local utility to provide multiple medium voltage circuits in a very short timeframe. A robust loop medium-voltage distribution system provides a high degree of maintainability and reliability. A bridge-power generation system was sourced by Summit and provided to ensure that utility timelines would not be an obstacle to hitting the end-customer’s demanding timelines for production. The bridge power system fed the campus-wide medium voltage distribution system designed by Summit.
The test floor comprises a 70-position liquid-cooled line at 176 kW per rack and a 192-position line at 104 kW per rack, both served on CDU secondary loops fed from a chilled-water primary system. Utility service, central plant and TCL distribution were sized to the facility’s full 60 MVA program capacity from the outset.
Customer identity, site designation and product line are confidential and have been omitted in accordance with the terms of Summit’s engagement.
Complex Design Requirements
- Two-tier liquid-cooling architecture — a 176 kW/rack line and a 104 kW/rack line — both served from a shared chilled-water primary plant through independent CDU secondary loops
- Humidity-controlled SMT environment coordinated with four parallel SMT lines and dedicated processor-board oven/X-ray inspection stations
- Utility service, central plant and TCL distribution engineered up front to the facility’s full 60 MVA build-out rather than phased in later
- Coordination of manufacturing, sub-assembly and rack-test floors within a single greenfield building envelope
Summit Delivery — Responsiveness That Drives Customer Success
As a ground-up greenfield delivery, this program depended on Summit’s design team keeping pace with an aggressive construction schedule from permit through startup. Summit’s responsiveness in resolving equipment coordination and lead-time risk in real time — developing sourcing options for critical MEP equipment and steel — kept manufacturing and test-floor construction moving in parallel rather than in sequence.
That dedication to schedule, paired with Summit’s attention to the fine coordination a mixed manufacturing-and-test facility requires, is what allowed this customer to bring both floors online together and hit their production start date.
Engineering Capabilities
Mechanical
- Chilled-water central plant with primary and CDU secondary loops serving both liquid-cooled test lines
- Humidity-controlled SMT room with dedicated conditioning equipment
- Dedicated oven and X-ray inspection station mechanical support on the processor-board lines
- Central plant sized to the facility’s full 60 MVA program capacity
Electrical
- 60 MVA utility service supporting four SMT lines, two processor-board lines, rack-level assembly stations and both test lines
- Dedicated per-rack power distribution and safety interlocks for 262 test positions up to 176 kW each
- Motor control centers and VFD-driven pump arrays for the central plant
Plumbing
- Stainless-steel TCL distribution from CDU secondary loops to each rack position, with per-rack manifolds, flushing provisions and instrumentation
- Compressed air, DI water and process utilities distributed to SMT, assembly and test areas
- Chilled-water piping and terminations coordinated with the customer’s CDU secondary-side equipment
Technology
- BMS integration of chiller-plant and CDU points with the customer’s test-rack cooling control system
- Sequences of operation and points lists developed for phased manufacturing-to-test commissioning
- Per-rack flow, temperature and differential-pressure monitoring wired to the test-rack cooling control system
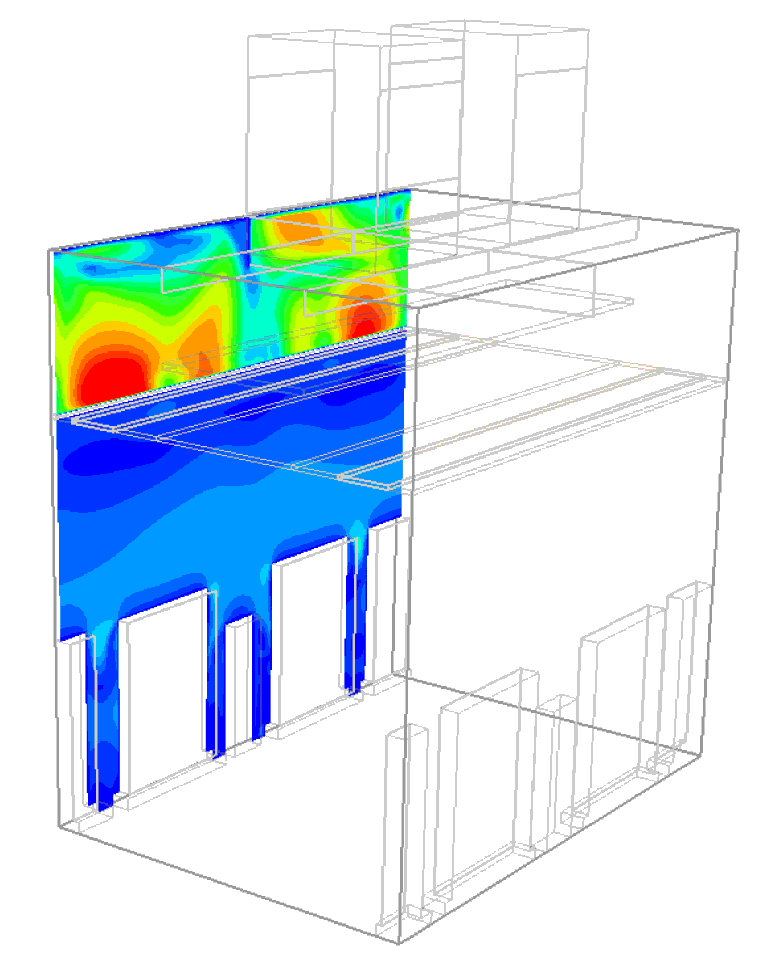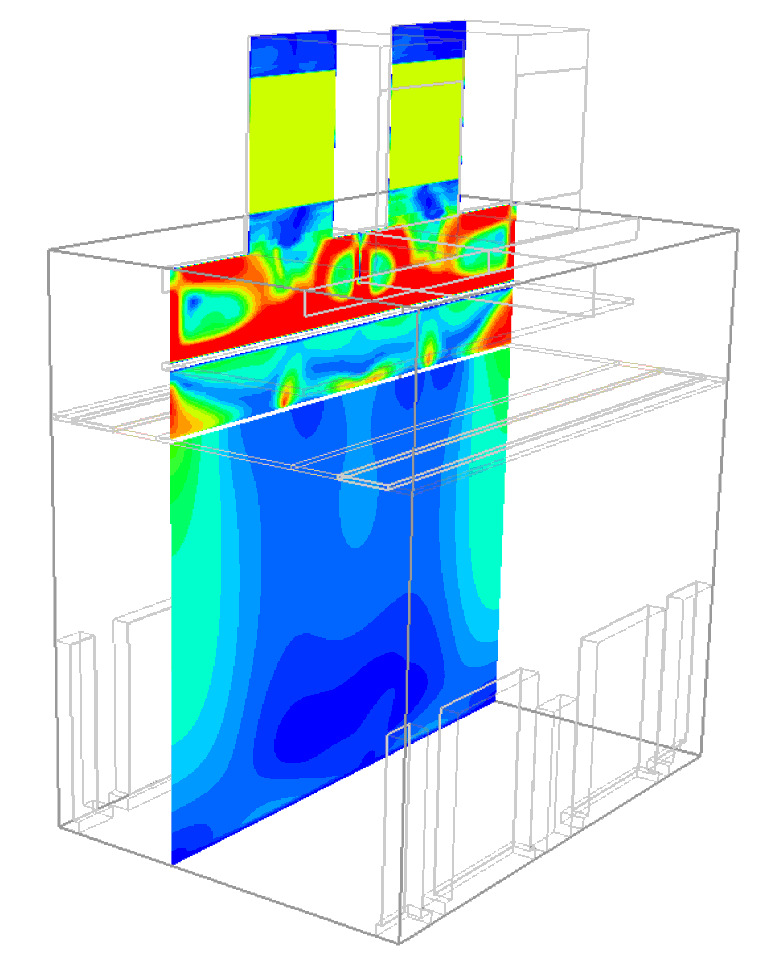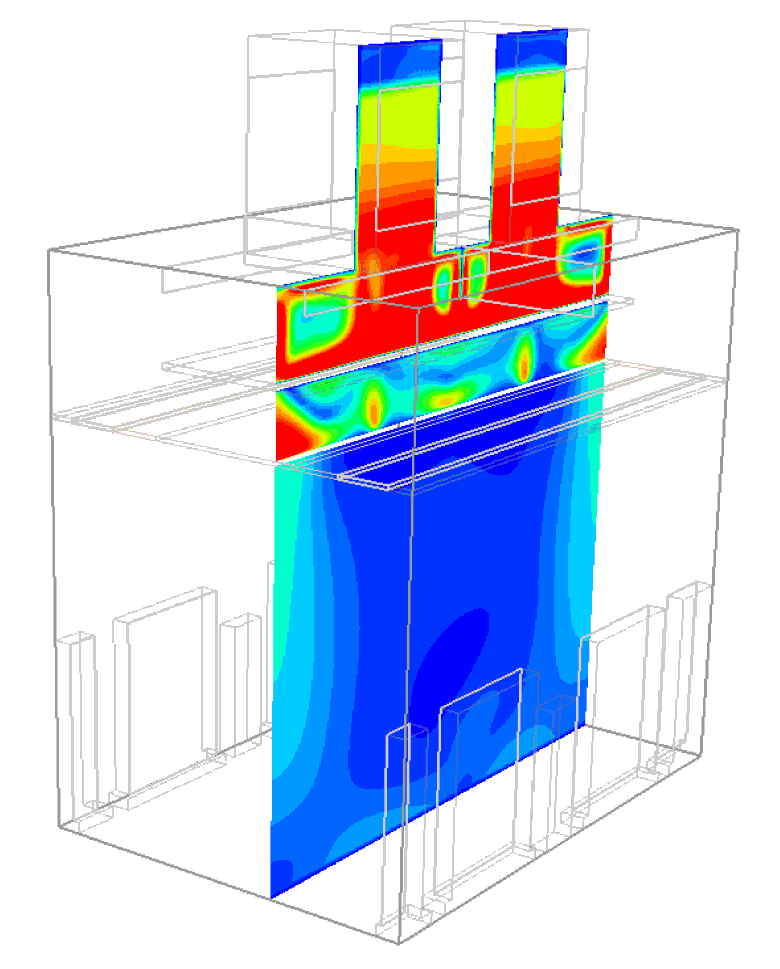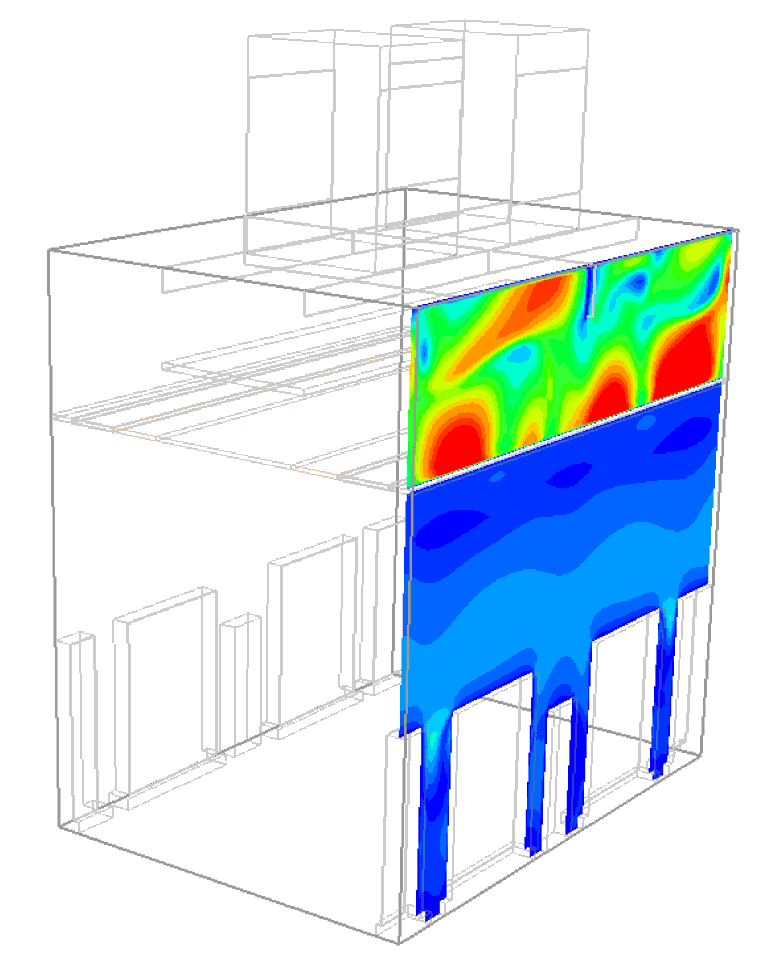
Note: Images are stock images not from the subject project to comply with non-disclosure requirements of the client.